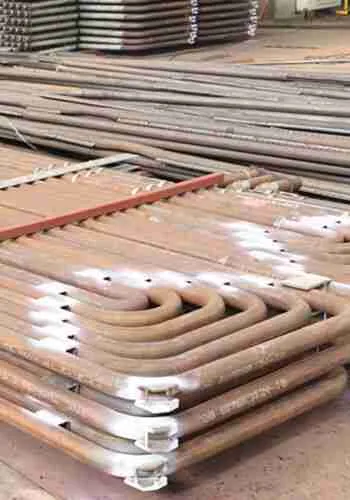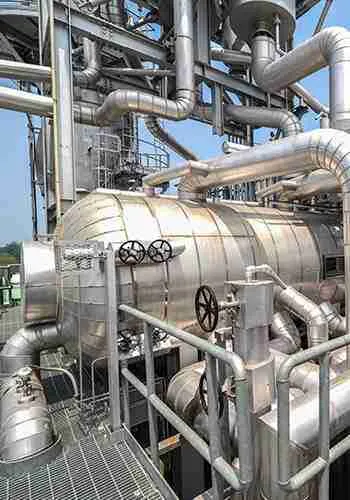
The boiler hydrostatic test (also known as a boiler pressure test) is an essential procedure to verify the strength, tightness, and safety of boiler pressure components. It ensures the reliability of the boiler before operation or after major maintenance, preventing potential failures during service.
This article provides a comprehensive overview of the requirements, test procedures, and safety precautions for performing a boiler hydrostatic test according to industrial standards.
1. Requirements for Boiler Hydrostatic Test
1.1 Test Categories
Boiler hydrostatic tests are generally divided into two types:
- Working pressure test, conducted at the boiler’s rated working pressure.
- Overpressure test, conducted at 1.25 times the rated drum pressure for the main boiler (including the superheater) and 1.5 times the rated inlet pressure for the reheater.
1.2 When Overpressure Testing Is Required
An overpressure test should be performed in the following cases:
a. Before the initial operation of a newly installed boiler.
b. After major repairs, replacements, or structural modifications of pressure parts.
c. Every six years for operating boilers, typically conducted after a major overhaul.
1.3 When Working Pressure Testing Is Required
A working pressure hydrostatic test should be conducted:
a. After routine or emergency maintenance.
b. Before restarting a boiler that has been idle for over 30 days.
c. For reheater systems only under special conditions, with approval from the Chief Engineer.
1.4 Standards and Documentation
All hydrostatic tests must comply with the “Supervision Regulation on Safety Technology for Power Industry Boilers and Pressure Vessels.”
Each test must have an approved plan and risk assessment signed by the Chief Engineer.
1.5 Personnel and Instrumentation
- The test should be directed by the operating supervisor, with two trained operators responsible for pressure control and gauge monitoring.
- At least two calibrated pressure gauges (accuracy 0.5 class or higher, range up to 40 MPa) should be installed—one at the upper drum and one at the control room—to ensure consistency.
2. Scope of Hydrostatic Test
- First circuit: Includes feedwater piping, economizer, steam drum, downcomers, water walls, superheater, main steam piping, and connected headers.
- Second circuit: Includes cold reheat and hot reheat piping, reheater, and associated headers.
- Auxiliary systems: Drain, vent, and instrument lines are tested up to the second valve.
- Safety valves and level gauges: Participate only in working pressure tests, not in overpressure tests.
3. Pre-Test Inspection and Preparation
Before testing, ensure:
- All mechanical work on steam and water systems is completed and work permits are closed.
- No personnel remain inside the furnace or flue gas path.
- Pressure gauges and level indicators are properly calibrated and functional.
- The water used is deionized or treated feedwater, meeting test quality requirements.
- Measures are in place to prevent turbine water ingress.
- All discharge and drainage valves operate smoothly.
- Communication between field personnel and the control room is established.
4. Hydrostatic Test Procedure
- Filling the boiler – Begin filling with feedwater pump until the water level is visible in the steam drum (approximately -100 mm).
- Air venting – Open air valves until a steady stream of water flows out, then close in sequence.
- Pressurization – Increase pressure slowly:
- ≤ 0.3 MPa/min until 10 MPa,
- then ≤ 0.2 MPa/min beyond 10 MPa.
- Intermediate checks – Pause at 10% and 80% of the lowest set safety valve pressure to check for leaks.
- Full pressure test – Maintain the working pressure for 5 minutes and observe pressure drop and any leakage.
- Overpressure test (if required) – Increase to test pressure (1.25× or 1.5× rated), hold for 5 minutes, then depressurize gradually at 0.2–0.3 MPa/min.
- Final inspection – When the pressure drops back to working pressure, check all welds and pressure components for leaks.
- Depressurization and drainage – Slowly release pressure through drains, open all air vents at 0.2 MPa, and drain remaining water after the test.
5. Acceptance Criteria
A hydrostatic test is considered qualified if:
a. The pressure drop is ≤ 0.1 MPa/min for the boiler body and ≤ 0.05 MPa/min for the reheater.
b. No visible leaks, misting, or sweating occur on pressure-bearing parts or weld seams.
c. No residual deformation or abnormal expansion is observed.
6. Safety and Precautions
- The test must be supervised by the maintenance manager with both operations and maintenance staff present.
- Conduct the reheater test before the main boiler and superheater tests.
- Adjust the water flow smoothly—avoid rapid opening or closing of valves to prevent water hammer.
- Maintain water temperature between 30°C and 50°C, and never below 21°C.
- Filling time should not be less than 4 hours in winter or 2–3 hours in other seasons.
- No personnel should approach pressure parts during overpressure testing.
- Pressure readings must be based on the drum or reheater’s calibrated local gauge.
- Handle and discharge high-alkalinity test water safely to avoid corrosion or environmental contamination.
- Record all test parameters, observations, and issues for documentation and future inspection.
✅ Conclusion
A boiler hydrostatic test is a crucial step in ensuring the safety and performance of pressure-bearing equipment. Strict adherence to standards, careful pressurization control, and accurate instrumentation are essential to avoid damage and ensure reliable operation.
By following these guidelines, DHB Boilers ensures that every boiler delivered to clients meets international safety and performance standards — ready for efficient, long-term operation.